
 Address:
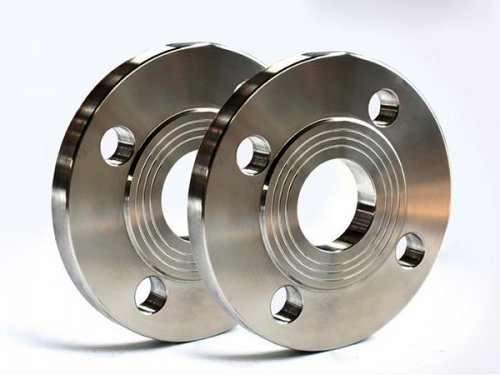
How to install stainless steel flat welding flange normally
The accessories on one side of the stainless steel flat welding flange are customized, and the fixture needs to reach the leakage point first. The key is to establish a closed cavity between the stainless steel flange of the valve body and the pipeline connection joint. In order to prevent leakage between the valve body and the stainless steel flange due to pressure maintenance, an annular cavity is set at the overlapping position of the clamp and the outer edge of the stainless steel flange of the valve body. The tooth contact clamp is used as a limiting device because during the injection process, the fixture on the small diameter stainless steel flange is easily moved to the small diameter stainless steel flange. After the sealant hardens during operation, check the stress relaxation effect, and then perform local re injection to close the injection port
Installation steps for stainless steel flat welding flanges
1. The welding current should not be too high, about 20% lower than that of carbon steel welding rods. The arc should not be too long, and interlayer cooling cannot prevent heating and corrosion of the flange cover
2. The electrode needs to be dried before use. Calcium titanium type should be dried at 150 ° C for 1 hour, and low hydrogen type should be dried at 200-250 ° C for 1 hour (do not repeat drying more than once). Do not increase welding, the carbon content of welding is to prevent electrode coating from adhering to oil and other dirt, so as not to affect the quality of the parts.3. When welding stainless steel flange fittings, carbides will precipitate and mechanical properties will be affected due to repeated heating and corrosion resistance.
4. After welding, the flanges of hardenable American standard chromium stainless steel flange fittings are larger and more prone to cracking. Similar types of chromium stainless steel electrodes (G202, when using G207) need to be preheated to 300 ° C or higher after welding. And gradually cool to about 700 ° C after welding. If heat treatment cannot be performed on the weld seam, rods (A107, A207) are required for welding stainless steel flange pipes
5. Stainless steel flange, with appropriate stabilizing elements such as Ti, Nb, Mo, etc., to improve its weldability based on actual reports. Weldability is better than that of chromium stainless steel flange. When using the same type of chromium stainless steel flange electrode (G302, G307), preheat it to 200 ° C or higher and temper it to about 800 ° C after welding. If not, it needs to be used 6. Stainless steel flange pipe welding rods (A107, A207), stainless steel flange pipe fittings, and butt welded flange electricity have excellent reporting and oxidizing properties and are widely used in the manufacturing of chemicals, fertilizers, petroleum, and diagnostic and therapeutic machinery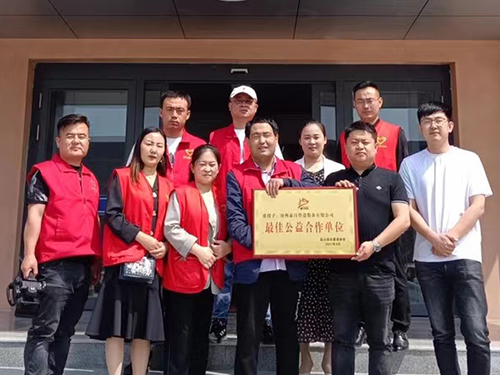
Taichang Foundation, Dedication in Action
Superior care promotes the development of Taichang Group
Taichang Achieves Every Struggler
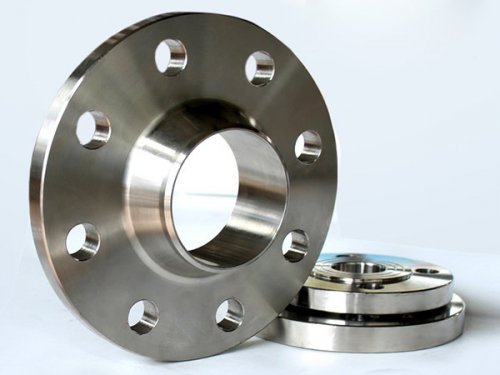
Introduction to Cleaning Knowledge of Carbon Steel Flanges
Explain the advantages of heat treatment process for carbon steel elbows
How to install stainless steel flat welding flange normally